Mechanical Assembly: Methods, Steps, and Quality
/ Uncategorized / By
When an assembled product rattles, leaks, or wears out early, the root cause may be a small detail: a loose fastener, a misaligned shaft, or a joint that doesn’t suit the materials. Mechanical assembly has a direct effect on how products perform and how reliably teams can produce them. Good results start with practical design choices, such as accessible fasteners, suitable tolerances, and features that guide parts into position. They also depend on clear work instructions, properly maintained tools, and checks at the right points in production. Learn how these elements fit together and what to consider when planning assembly for a new or existing product.
Key Takeaways
- Select joining methods to fit the job: Consider materials, expected loads, production volume, and whether the assembly needs to be serviced.
- Design with assembly in mind: Set practical tolerances, plan the build sequence, and allow access for tools, inspection, and maintenance.
- Coordinate production and quality checks: Use clear instructions, inspect components and joints throughout assembly, and align mechanical and electronic work early.
What Is Mechanical Assembly?
How assembly turns components into products
Mechanical assembly joins separate components to create a working product or subassembly. It often follows the fabrication of individual parts and may be one of the final stages of production. A technician might fasten a cover to a housing, fit gears into a gearbox, or attach brackets to a frame. Each connection needs to meet the design requirements so the finished assembly performs as intended.
The process can involve screws, press fits, adhesives, or other joining methods. The right choice depends on the design, materials, and expected use. Clear work instructions also help teams assemble parts in the correct order and handle them consistently. Mechanical assembly methods range from simple manual tasks to repeatable production-line operations.
How assembly affects performance, reliability, serviceability, and cost
Assembly choices influence how well a product performs and how long it lasts. A misaligned shaft, loose fastener, or weak joint can lead to vibration, leaks, or early failure. Selecting suitable joining methods and following a consistent process helps components stay in position under expected loads and operating conditions.
Assembly decisions also affect maintenance and production costs. When technicians can reach fasteners or replace worn parts without dismantling an entire product, repairs can be simpler. Unnecessary components and complex steps, on the other hand, may add labor, inspection, and rework. In-process checks help identify problems before they carry through production. Effective quality control practices help manufacturers track consistency and address defects before products reach customers.
How mechanical assembly connects to electronic assemblies
Mechanical assembly often describes products or subassemblies without electronics, such as a valve body, enclosure, or frame. When a product combines mechanical parts with circuit boards, motors, sensors, or wiring, it is commonly called an electromechanical assembly. The mechanical structure needs to support and protect electronic components while leaving room for them to operate as designed.
This requires mechanical and electronic requirements to be considered together. An enclosure, for example, may need accurately positioned openings for connectors, mounting points for a PCB, and space for cable routing. Addressing these details during design can help prevent fit issues during production. For manufacturers sourcing both mechanical and electronic work, integrated manufacturing services can coordinate components such as molded plastics, machined parts, PCB and cable assemblies, and final assembly with engineering and program management support.
Which Joining Methods Does Mechanical Assembly Use?
Mechanical assemblies use removable joints, permanent joints, or a mix of both. The right method depends on the materials, expected loads, production volume, and whether the product may need maintenance or repair. A well-chosen joint keeps parts in position while supporting reliable production and service.
Threaded fasteners: screws, bolts, and nuts
Screws, bolts, and nuts create strong joints that can usually be taken apart. They work well when a product needs inspection, repairs, replacement parts, or reconfiguration. Screws can secure panels and brackets, while bolts and nuts often join components that require a firm clamping force.
Fastener selection should account for the materials, expected loads, vibration, tool access, and required torque. Overtightening can damage a part or strip its threads; insufficient torque can allow components to shift. Clear work instructions and properly set tools help make each joint consistent. Fischer ASIA’s guide to mechanical assembly covers common fasteners and other joining methods.
Press fits, interference fits, and snap-fits
Press and interference fits hold parts together through friction. One component is slightly larger than the opening it enters, creating pressure between the surfaces when the parts are assembled. These fits are common for pins, bushings, and bearings. Dimensions and material properties need close control: an overly tight fit can deform or crack a part, while a loose fit may not hold securely.
Snap-fits use a flexible feature that bends during assembly, then returns to hold another part in place. Often molded into plastic housings, they can reduce the need for separate hardware. Designers should consider the material’s flexibility, assembly force, and whether the joint may need to be opened again. Komaspec’s overview of mechanical assembly methods describes these options and their uses.
Riveting, welding, and brazing
Riveting creates a permanent mechanical joint by deforming a rivet to hold parts together. It is commonly used with sheet metal and can join components without threaded hardware. Since removing a rivet can damage it or the surrounding material, consider repair and access needs before choosing this method.
Welding joins materials using heat, while brazing uses a filler material to connect parts without melting the base materials. Both can form durable joints for products such as frames and enclosures. The best option depends on material compatibility, joint design, strength requirements, and production conditions. Heat may affect nearby components or change material properties, so the process and assembly sequence need careful control. Komaspec explains these permanent joining methods.
Adhesive bonding
Adhesives can join different materials, spread loads across a joint, and help seal against moisture or contaminants. Bonding can be useful when fasteners would add weight, take up space, or create stress points. The adhesive must suit the materials and the product’s operating conditions, including temperature, chemical exposure, and vibration.
Surface preparation matters: oil, dust, and residue can weaken a bond. Parts may need cleaning or treatment before adhesive is applied, and curing time can affect the production schedule. Because bonded joints can be difficult to inspect or separate, plan how the process will be monitored and how defects will be detected. Adhesive bonding works best when it is built into the design and assembly plan from the start.
How materials, loads, volume, and service needs guide method selection
Begin by defining what the joint must withstand and how the product will be used. Consider the materials, the direction and size of expected loads, and exposure to heat, moisture, chemicals, or vibration. A plastic housing may be suited to snap-fits, while a metal bracket that needs regular servicing may call for bolts.
Production volume also matters. A method that is practical for a small batch may need different tooling or automation at higher volumes. Consider whether technicians will need to open the product, replace parts, or perform repairs. Permanent joints can provide durable connections, while removable fasteners support service access. Eigen Engineering’s assembly guide outlines how product purpose and operating conditions inform method selection. EMS Technologies can also coordinate assembly with tooling and component production.
How Does the Mechanical Assembly Process Work?
A dependable mechanical assembly process follows a defined plan, from reviewing product requirements to checking the finished assembly. Each step helps teams confirm that components fit, joints meet specifications, and the product performs as intended. The process varies by product, but clear instructions and consistent checks help reduce defects, avoid rework, and keep production on schedule.
Assembly also depends on how well different parts of manufacturing work together. A product may combine molded, stamped, machined, or cast components with PCB and cable assemblies. Coordinating those parts requires communication between engineering and production teams. A manufacturing partner with integrated capabilities, such as EMS Technologies, can support mechanical and electronic production within a larger manufacturing program.
Review requirements, drawings, tolerances, and assembly sequence
Before production begins, engineers and assembly teams review product requirements, drawings, specifications, and tolerances. They check how parts fit together, whether fasteners are accessible, and whether the proposed assembly sequence is practical. This review can uncover issues such as a component blocking access to a screw or a tolerance that makes a consistent fit difficult.
The team also identifies special tools, inspection points, and handling requirements. Clear work instructions explain the order of operations and help assemblers follow the same process. Reviewing the design early can reveal fit and access concerns before they disrupt production. Eigen Engineering’s guide to mechanical assembly also emphasizes checking drawings and specifications for potential assembly problems.
Prepare components and check for defects or variation
Before assembly, teams check that components are clean, complete, and within specification. Dirt, burrs, and machining residue can interfere with fit or damage a surface. Some parts may also need lubricant, a coating, or sealant before they are assembled. Preparation requirements depend on the materials, joining method, and product design.
Incoming inspection helps catch defects and variation before parts reach the assembly station. Teams may measure critical dimensions and check surfaces against the drawing or specification. If a component does not meet requirements, they can set it aside for review rather than pass it into production. This early check helps prevent a component issue from affecting later steps or requiring rework after the product is assembled.
Position parts with jigs or fixtures and confirm alignment
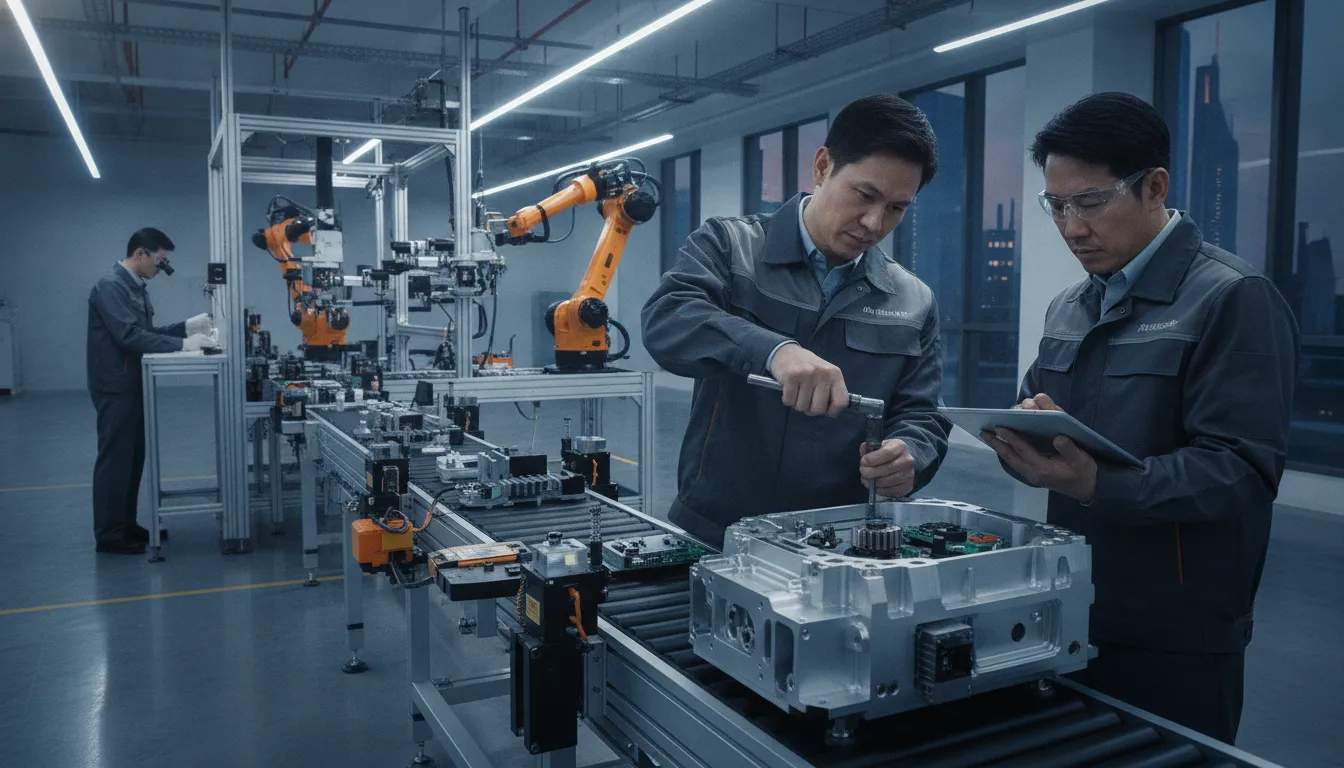
Assemblers position parts according to the product design and work instructions. Jigs, fixtures, and locating pins can hold components in place and help maintain alignment as the assembly progresses. These tools are useful when a product has several parts or requires repeatable positioning across production runs.
Before joining components, assemblers check that parts sit correctly and that holes, edges, or other reference features line up. A part that shifts or sits at the wrong angle can affect fit, function, or appearance. The right fixture gives the team a stable setup for the next operation and can make positioning more consistent. Teams should also confirm that the fixture is suitable for the parts being assembled and does not damage or distort them.
Join components with specified tools, settings, and work instructions
Once components are positioned, assemblers join them using the method specified for the product. Common methods include threaded fasteners, press fits, welding, and adhesive bonding. Work instructions should identify the required tools, settings, sequence, and handling steps so that each joint meets the design requirements.
For a fastened joint, the specified torque helps create a secure connection without loosening or damaging components. Other methods may require controlled heat, pressure, or curing time. Following documented procedures helps reduce variation between operators and production runs. Teams should verify critical tool settings and maintain equipment according to the production plan. When a joining step is sensitive to small changes, a clear process and properly maintained tools help make results more repeatable.
Inspect, test, and document the assembly
Inspection can take place during assembly and after the product is complete. In-process checks help confirm dimensions, alignment, surface condition, and fastener installation while issues are still easier to address. Final inspections verify that the finished assembly meets its specifications.
Testing should reflect the product’s requirements. Depending on the design, teams may check fit, movement, connections, or operation under expected conditions. They record inspection results, test outcomes, and corrective actions to create a traceable account of the work. That documentation supports quality reviews and helps teams investigate recurring problems. If a defect appears, records can help identify where it occurred and whether the cause relates to a component, tool, instruction, or assembly step.
How Can Design Prevent Assembly Problems?
Assembly problems often begin before production, when a design makes parts difficult to position, join, inspect, or service. Reviewing assembly needs early helps teams make practical choices about components, tolerances, joining methods, and production steps. These decisions can reduce rework and help create a more repeatable process.
Apply design-for-assembly principles early
Consider assembly while the product is still being designed, not after tooling and production plans are in place. For each component, ask how it will be positioned, joined, inspected, and removed if the product needs service. The best joining method depends on factors such as material, strength requirements, operating conditions, and whether the joint must be removable. Design-for-assembly principles help teams weigh these needs before design choices become production constraints.
Involve manufacturing and assembly teams in design reviews. They can identify hard-to-reach joints, difficult assembly sequences, and processes that call for specialized equipment. EMS Technologies brings engineering and manufacturing services together to support projects from design through production.
Reduce unnecessary parts, joints, and steps
Every component must be made or sourced, handled, positioned, and joined. Extra parts can add labor and create more opportunities for fit issues or assembly errors. Review the bill of materials and ask whether each part needs to move independently, use a different material, or remain separate for assembly or maintenance. If not, consider whether it can be combined with another component.
Fewer parts are not always better if combining them makes repair or replacement more difficult. The goal is to simplify the design without compromising function or serviceability. A mechanical assembly review can help identify opportunities to reduce parts and steps while preserving product requirements.
Set practical tolerances and clear datums
Tolerances define the acceptable variation in a part’s dimensions. If tolerances are too loose, parts may not align or joints may not hold as intended. If they are tighter than the product’s function requires, manufacturing and inspection may become more demanding. Set tolerances according to how parts fit, move, seal, or carry loads in the finished product.
Datums are reference surfaces or points used to measure and position features. Clear datums give design, manufacturing, inspection, and assembly teams a shared reference. Also check how dimensional variation can accumulate across multiple parts, especially at critical interfaces. Assembly guidance can help teams account for product use and maintenance when setting requirements.
Provide access for tools, inspection, and maintenance
Check that assemblers can reach joints with the required tools, such as drivers, wrenches, or presses. Allow enough clearance to hold components securely during joining, and consider the assembly sequence: a part installed early should not block access to fasteners or connections needed later.
Plan access for inspection and service, too. Quality teams need to reach critical joints, while maintenance staff may need to remove components without damaging nearby parts. In-process checks can catch issues while components are still accessible; final checks can confirm functions such as sealing or latch operation. Quality control practices can help teams place inspections at useful points in the process.
Design features for alignment and safe handling
Small positioning errors early in assembly can affect later steps. Features such as pins, slots, tabs, and molded guides can help parts fit together in the intended position. Make orientation clear, and avoid designs that allow a component to be installed incorrectly when possible. Jigs and fixtures can hold parts steady and support repeatable assembly.
Consider how people or equipment will lift, grip, and position each component. Account for part weight and balance, provide room for hands or handling equipment, and avoid sharp edges where practical. Check that locating features and fixtures suit the planned assembly sequence. Mechanical assembly guidance emphasizes confirming alignment before joining, since an early positioning error can carry through the process.
What Challenges Affect Mechanical Assembly?
Mechanical assembly depends on parts fitting and working together as intended. Dimensional variation, material choices, and inconsistent work methods can all affect the finished product. When teams address these risks early, they can reduce avoidable rework and keep quality, schedule, and cost in view.
Misalignment and tolerance stack-up
Every component has dimensional tolerances, and small variations can accumulate as parts are assembled. This tolerance stack-up may leave holes out of position, create uneven gaps, or prevent components from fitting together as designed. Misalignment can also place extra stress on fasteners and joints, which may affect performance and reliability over time.
Clear datums, practical tolerances, and features that guide parts into position can help reduce these risks. Teams can also check critical dimensions before assembly and use fixtures to hold parts consistently. As Lectronix explains in its quality control overview, unnoticed manufacturing variations can delay validation, increase costs, and affect product reliability after release.
Material incompatibility and joint failure
Materials that perform well on their own may not work well together. Differences in strength, stiffness, thermal expansion, or corrosion resistance can affect how a joint holds up under load or changing temperatures. A fastener may loosen, an adhesive may fail to bond as expected, or contact between dissimilar metals may cause corrosion.
Select materials and joining methods based on operating conditions, expected loads, and service life. Validate critical joints before production, then check them during assembly rather than relying only on final inspection. Building quality checks into the process helps teams spot problems closer to their source. SixSigma.us’ manufacturing quality guidance also recommends integrating quality into production instead of relying solely on late-stage checks.
Component variation and inconsistent work methods
Parts from different production runs or suppliers may vary in dimensions, finish, or fit. Even when components meet their individual specifications, these differences can make assembly harder or produce inconsistent results. Variations in how workers position parts, apply adhesives, or tighten fasteners can add to the challenge.
Incoming inspections can identify component issues before they reach the assembly line. Clear work instructions, acceptance criteria, and training help assemblers follow the same sequence and technique. Mitti’s guide to manufacturing quality control describes routine inspections as a way to detect and correct defects or variations during production. Teams can also share inspection findings with suppliers to address recurring problems and improve consistency over time.
Rework and delays from late defect detection
When a defect appears only during final inspection, fixing it may require disassembling components, replacing parts, or repeating tests. This rework takes time and can delay delivery, especially if an issue affects multiple units or requires a hard-to-source component. Late detection can also make it more difficult to trace the cause.
In-process checks help catch issues while the assembly is accessible and easier to correct. Teams might verify alignment before fastening or inspect a joint before adding covers. Statistical process control can reveal trends in measurements and production results. Amrep Inspect’s overview of quality control methods explains how identifying small variations early can help prevent costly errors and production delays.
Balance speed and cost with product requirements
The fastest assembly method is not always the right one. Manual assembly may suit low-volume products or designs that change often, while automation can support repetitive or precision-dependent tasks at higher volumes. The choice depends on product complexity, quality requirements, production volume, and the cost of equipment and maintenance.
Compare the full process, including setup, labor, inspection, and the potential cost of defects, rather than focusing on cycle time alone. Pilot runs can show whether a method meets requirements before it is used at scale. Autodesk’s overview of manufacturing automation describes potential gains in efficiency, productivity, and error reduction. EMS Technologies offers integrated manufacturing services with engineering and program management support to help coordinate production needs.
Which Practices Improve Assembly Efficiency and Quality?
Efficient assembly is not simply a matter of moving faster. Clear instructions, skilled assemblers, dependable equipment, and useful process data help teams build products consistently and catch problems before they lead to rework. The right practices also depend on the product, production volume, and quality requirements.
Standardize work instructions and assembly sequences
Create step-by-step instructions that identify the correct parts, assembly order, tool settings, torque requirements, inspection points, and safety precautions. Photos or diagrams can help show component orientation and how parts should fit together. Keep instructions current when a drawing, component, or process changes, and make sure assemblers can find the latest approved version.
A consistent sequence reduces variation between operators, shifts, and production runs. Include checks at key stages so teams can identify issues before an assembly is complete. For example, a combination of solder paste inspection, optical inspection, and functional testing can help detect problems during PCB assembly. Lectronix explains how these methods support quality control in PCB assembly.
Train assemblers on tools, procedures, and quality requirements
Train assemblers to use equipment, handle components, follow work instructions, and check critical features. Hands-on practice can help employees become comfortable with a task before they perform it independently. Provide refresher training when procedures change, and confirm understanding by observing the task or asking team members to demonstrate it.
Training should also explain what to do when a part or process falls outside requirements. Make it easy for employees to report defects, ask questions, and flag instructions that are unclear. Assemblers often notice recurring issues because they work directly with the process. Regular training in equipment use, inspection techniques, and quality standards helps build those skills, as outlined in this guide to manufacturing quality control.
Use jigs and fixtures for repeatable positioning
Jigs and fixtures hold components in a consistent position during assembly, fastening, or inspection. They can reduce reliance on visual judgment and make alignment easier, particularly when parts are small, heavy, or difficult to hold by hand. For example, a fixture can keep a bracket square while an assembler installs fasteners.
Design these aids around the part and task. They should make correct placement straightforward, prevent common orientation errors, and leave enough room for tools and inspection. Sensors or go/no-go checks can provide another safeguard by preventing work from continuing if a part is missing or incorrectly positioned.
Inspect fixtures for wear, damage, or buildup. A worn locating surface can introduce variation rather than prevent it. Komaspec describes how fixtures help hold and locate components in its guide to mechanical assembly methods.
Calibrate torque tools and maintain equipment
Fasteners need the correct torque to hold securely without damaging threads, deforming parts, or creating uneven clamping. Specify torque settings in the work instructions, use calibrated tools, and follow the required calibration schedule. When torque verification is part of the product’s quality requirements, record the results so they can be reviewed.
Regular equipment checks also help keep assembly consistent. Look for worn or damaged tools, loose connections, and other issues that could affect performance. Set a maintenance schedule and explain how operators should report problems or remove faulty equipment from use.
Planned maintenance can reduce unexpected equipment failures and interruptions to production. Total Productive Maintenance involves employees in routine upkeep to support equipment reliability. Amrep Inspect discusses this approach as part of its overview of quality control methods.
Automate repetitive or precision-dependent tasks
Automation can help with tasks that happen repeatedly, require precise movement, or need consistent application. Depending on the product and production volume, examples may include fastening, adhesive dispensing, component placement, or functional testing. Automating a suitable task can reduce manual variation and allow employees to focus on work that calls for judgment or specialized skills.
Start by assessing the task and production needs. Consider volume, part variation, changeover requirements, equipment costs, and how the process will be inspected. A well-designed manual process may be more practical for low-volume work or products that change often.
Before adopting automation, test it with representative parts and decide how operators will monitor performance. Automation is most useful when the process is understood and the equipment fits the work. Autodesk discusses the role of data in manufacturing automation.
Review process data and feedback to find improvements
Track measures that help explain how assembly is performing, such as first-pass yield, defect types, rework, cycle time, downtime, and inspection results. Reviewing these measures over time can reveal recurring issues and help teams distinguish an isolated problem from a process trend. Share the information with the employees who can act on it.
Combine data with feedback from assemblers, inspectors, and engineers. A rise in rework, for instance, may point to unclear instructions, a fixture that needs attention, or variation in an incoming component. Investigate the likely cause, test a change, and confirm that it improves results before making it standard practice.
Record corrective actions and follow up to see whether the fix lasts. Manufacturing data can help teams identify ways to improve efficiency and reduce downtime, as described in this overview of industrial automation. When a program involves mechanical and electronic components, an integrated manufacturing partner such as EMS Technologies can coordinate engineering and production services.
How Do Quality Checks and Safety Practices Support Reliability?
Reliable mechanical assembly depends on more than a final inspection. Teams need to confirm that components meet specifications, assembly steps produce consistent results, and finished products perform as intended. Checks throughout production help catch issues when they are easier to address, before a small variation leads to rework, delays, or a product failure.
A practical quality plan starts with clear requirements. Drawings, tolerances, work instructions, and acceptance criteria give assemblers and inspectors a shared standard. The plan should identify which parts and process steps need attention, what measurement or test to use, and how to handle results that fall outside requirements. Consistent measurement and analysis help manufacturers track product characteristics and maintain standards across production, as explained in this guide to quality control in manufacturing.
Safety supports quality by helping employees handle tools, equipment, and materials correctly. Training and equipment maintenance can reduce workplace risks while also supporting steady production. This is especially important when an assembly combines mechanical components with electronics, where a problem at one stage can affect the broader product. EMS Technologies offers integrated manufacturing services spanning mechanical and electronic production, supported by in-house engineering and program management teams.
Inspect incoming components and verify critical dimensions
Incoming inspection confirms that components meet specifications before they enter assembly. Depending on the part, checks may cover visible damage, material condition, thickness, hole locations, length, or other dimensions that affect fit and function. Catching a mismatch early can prevent parts from being forced together, creating excess stress, or causing problems later in production.
Inspection criteria should come from product drawings, tolerances, and customer requirements. Teams can prioritize dimensions and characteristics that affect safety, performance, or the next assembly step. They should also record results in a consistent way, so recurring variation can be traced to a supplier, material batch, or manufacturing process. Accurate measurement helps manufacturers identify issues and maintain consistent standards throughout production, as outlined in this manufacturing quality control guide.
Check alignment, fastener torque, and joint integrity during assembly
Even parts that pass incoming inspection can be assembled incorrectly. During assembly, workers should confirm that components are oriented and aligned as specified, mating surfaces fit properly, and fasteners are tightened to the required torque. Fixtures and alignment features can help position parts consistently, while calibrated tools help reduce variation in tightening.
The right inspection depends on the joint. Threaded connections may require torque verification; press-fits may need checks for insertion force and final position. Welded, bonded, or riveted joints may call for visual inspection or other tests based on product requirements. Material and dimensional variation can affect joint strength, so teams should monitor critical characteristics during assembly. These quality control methods can help manufacturers spot variation before it affects product performance or safety.
Catch defects early with in-process checks
In-process checks give teams opportunities to find defects while production is underway, rather than waiting until the product is complete. Inspections can follow a critical joining step, take place at a workstation change, or happen before a component is covered or becomes difficult to reach. Finding a misplaced part early usually makes correction faster and avoids unnecessary disassembly.
Each check should have clear acceptance criteria that match the risks of the task. An assembler might verify part orientation, confirm that required fasteners are present, or measure a feature before moving to the next step. If the same issue appears repeatedly, teams can review the work instructions, tools, equipment, or incoming components involved. Routine inspections help identify defects and process variation before they compromise quality, as described in this overview of manufacturing quality control.
Test final dimensions and functions against requirements
Final inspection verifies that a completed assembly meets its specifications before release. Depending on the product, this may include visual checks, dimensional measurements, fit checks, movement tests, or functional testing. The test plan should reflect how the product is expected to work and identify the characteristics that matter most to its performance and safety.
Teams should define the inspection method, required equipment, and acceptable results in advance. For example, an assembly may need to move through a specified range, hold a load, or connect correctly with another component. Recording the results creates evidence that the product passed its checks and gives teams information to review if issues occur later. Final inspection and testing help confirm that products meet quality requirements before delivery, as explained in this guide to quality control.
Apply sampling or statistical process control when appropriate
Inspecting every feature on every unit may not be practical, particularly in higher-volume production. Sampling provides a planned way to check selected parts, while statistical process control (SPC) uses process data to monitor variation over time. The suitable approach depends on factors such as product risk, production volume, customer requirements, and how stable the process is.
A sampling plan should specify how many units to inspect, how often to check them, and what action to take when results fall outside acceptable limits. SPC can help teams identify process shifts before they create a larger number of nonconforming parts. It works best when teams respond to the data, investigate unusual patterns, and adjust the process when needed. Monitoring variation can help manufacturers detect problems early and reduce production errors, as described in these quality control methods.
Record inspection results, traceability, and corrective actions
Inspection records connect product requirements with production results. Depending on the process, records may include measurements, test outcomes, part or batch identifiers, inspection dates, and the equipment used. Traceability helps teams identify which components and production steps contributed to an assembly, making it easier to investigate a quality concern.
When a result falls outside requirements, teams should document how they contained affected product, what they found, and what corrective action they took. They should then verify that the action addressed the cause and did not create a new issue. Clear records support accountability, audits, and ongoing process improvement. Maintaining inspection, test, nonconformance, and corrective-action information gives teams a reliable history to review, as explained in this quality control guide.
Follow safe procedures for tools, equipment, and material handling
Safe work procedures help protect employees and support consistent production. Instructions should cover how to operate tools and equipment, handle heavy or awkward components, and manage hazards related to each task. Training helps employees follow the correct steps, while routine checks can identify damaged or worn equipment before it affects safety or assembly quality.
Equipment maintenance matters for reliability, too. Tools that are out of adjustment can produce inconsistent results, and equipment failures can interrupt production or create hazards. A planned maintenance routine helps teams keep equipment in good working order and address issues before they cause downtime. Total Productive Maintenance encourages employee involvement in equipment care to improve reliability, as described in these quality control methods. Safety procedures should reflect the actual tools, materials, and tasks used on the production floor, and teams should review them when processes change.
How Does Mechanical Assembly Fit into Integrated Manufacturing?
Mechanical assembly connects component design, production, and quality checks. When these steps are coordinated, teams can address fit and function early, before small issues become production delays.
Coordinate molded, stamped, machined, and cast components
A product may combine injection-molded housings, stamped brackets, machined shafts, and die-cast parts. Each process brings its own materials and tolerances, so teams need to consider how components fit together as a complete assembly.
A design change can affect several connected parts. Changing a shaft diameter, for example, may require updates to its bracket, seal, or coupling. Parametric models help teams track those relationships and update related features consistently, as explained in this guide to mechanical engineering software integration. Early coordination between engineering and production can reveal fit concerns before manufacturing begins. EMS Technologies offers molded plastics, metal stamping, machining, and die casting for projects that bring these processes together.
Integrate mechanical parts with PCB and cable assemblies
Products with electronics need mechanical structures that protect circuit boards, provide space for cables, and keep connectors and controls accessible. If mechanical and electrical components are designed separately, teams may find interference or access problems during assembly, when changes are more disruptive.
Cross-functional reviews help teams check clearances, mounting points, cable paths, and service needs before production. Quality checks also belong throughout the electronics process, not only at final inspection. Combining inspection methods with functional testing can help identify issues earlier, as outlined in this overview of PCB assembly quality control. A manufacturing partner with mechanical and electronic capabilities can coordinate these requirements across the product. That coordination supports a smoother handoff from component production to final assembly.
Connect engineering, tooling, production, and program management
Assembly starts long before parts reach the production floor. Engineering defines product requirements, tooling supports component production, and manufacturing teams follow approved processes. Program management coordinates schedules, communication, and changes across these activities.
When teams share information, they can resolve concerns before those concerns interrupt production. Assembly feedback, for instance, may show that a part needs a clearer alignment feature or more room for a tool. Automation can handle repetitive or precision-dependent tasks, while employees focus on work that calls for judgment. Autodesk’s overview of manufacturing automation describes how automation can streamline production and business processes. EMS Technologies highlights its engineering and program management support as part of its integrated manufacturing approach.
Assess a contract manufacturer’s assembly capabilities and quality processes
When assessing a contract manufacturer, ask how it reviews drawings and tolerances, controls assembly steps, and checks finished products. Find out how it manages design or process changes, and whether it can coordinate mechanical and electronic requirements if your product includes both.
Ask about inspection records, traceability, nonconforming parts, and corrective actions. It’s also useful to clarify which processes happen in-house and how the manufacturer works with outside suppliers. Effective quality controls help identify problems before products reach customers, as described in this manufacturing quality control overview. Compare the answers with your product’s complexity, volume, and service needs, then review the manufacturer’s available services to see whether they align with your project.
Related Articles
- What is Mechanical Assembly? Process, Types & Best Practices
- Mechanical Assembly Methods: A Complete Guide
- Mechanical Assembly: Methods, Tools, and Quality Control
- Quality Control in Manufacturing
- Quality Control in Manufacturing: A Complete Guide
Frequently Asked Questions
What is the difference between mechanical assembly and electromechanical assembly? Mechanical assembly joins parts such as housings, brackets, and shafts. Electromechanical assembly combines those parts with electrical or electronic components, such as circuit boards, motors, sensors, and cables.
How do manufacturers choose the right joining method? They consider the materials, loads, operating conditions, production volume, and whether the product needs to be serviced. A removable fastener may suit a product that requires maintenance, while a permanent joint may work better when parts should stay fixed.
What information should a manufacturer review before assembly begins? The team should review current drawings, specifications, tolerances, assembly sequence, inspection criteria, and any special tooling or handling needs. This can reveal fit or access concerns before they affect production.
How can a company reduce defects during mechanical assembly? Use clear work instructions, check incoming components, position parts with suitable fixtures, and inspect critical steps before the assembly is complete. Keep records of test results and corrective actions to help identify recurring issues.
What should I look for in a contract manufacturing partner? Look for experience with the processes your product needs, a clear approach to quality checks and traceability, and the ability to coordinate engineering with production. For products that combine mechanical and electronic components, EMS Technologies offers services such as molded plastics, machining, PCB and cable assemblies, and turnkey assembly, with in-house engineering and program management support.